Blow Molding vs Injection Molding: Process Differences
The blow molding process shapes hollow parts by inflating a molten tube, while the injection molding process packs material into a closed mold. Buyers should choose based on part geometry, wall thickness, cycle time, and tooling cost.
- The blow molding process forms hollow parts by inflating a preform tube, which suits containers, bottles, and large thin-wall items.
- The injection molding process packs molten material into a closed mold, which suits solid parts, thick walls, and high-precision features.
- Buyers should match the process to part geometry, wall thickness, cycle time, tooling cost, and material requirements.
- A clear spec sheet and sample evaluation help confirm the right process before tooling is ordered.
How the two forming methods work
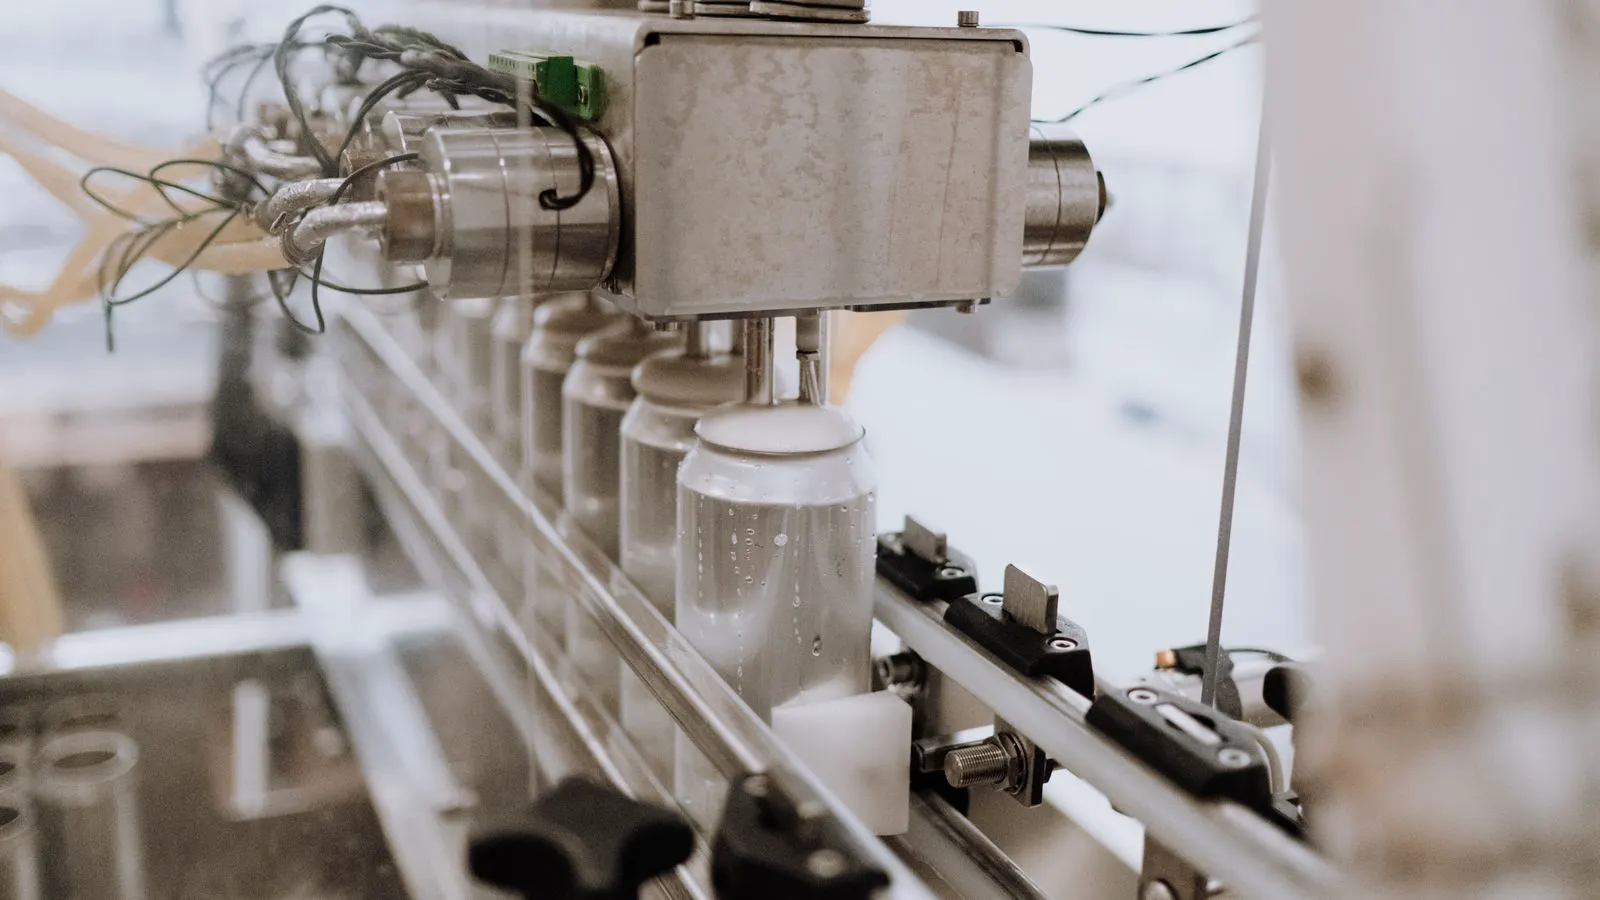
The blow molding process begins at the preform stage. A small amount of molten resin is shot into a mold and cooled into a solid tube. The tube has a long, narrow body and a short, thick neck. Once the preform cools to a workable temperature, a mold grip secures the neck. A blow molder then introduces air or nitrogen into the tube through the neck. The gas pressure forces the plastic tube to expand against the inner wall of the mold cavity. As the tube stretches, it thins out. The plastic cools against the mold surface, hardens into the shape of the cavity, and the mold opens to release the hollow part.
The injection molding process follows a different mechanical path. A hopper feeds plastic pellets into the heated barrel of the machine. A rotating screw or a piston compresses and melts the material. The molten plastic is pumped at high pressure into a closed mold cavity. The material fills the space, packs against the walls, and fills the corners of the cavity. Once the cavity is full, the machine holds the pressure to prevent shrinkage. The plastic cools and solidifies. The mold opens, and an ejection system pushes the part out.
Both processes rely on heat and pressure to shape thermoplastic resin. The fundamental difference lies in how the cavity is formed. Blow molding creates the cavity by expanding a tube against a mold wall. Injection molding fills a pre-shaped, finished cavity with molten material.
Part shape and wall thickness
Hollow parts are the primary driver for blow molding. Containers, bottles, jugs, tanks, and large thin-wall parts suit the blow molding process because the plastic sheet thins evenly as it expands. The process is particularly effective for parts with large surface areas and relatively low wall thickness.
Injection molding works best for solid parts or parts with thick walls. It also handles fine details, threads, ribs, and undercuts that blow molding struggles to form. Injection molds can capture complex geometries that are difficult to achieve by stretching a tube.
A thin-walled bottle is a good example. The blow molding process stretches the molten plastic into a large area with little material. The wall stays thin. The same bottle shape would be difficult to make in a standard injection mold because the cavity would need to be hollow from the start, and the part would need strong supports to hold the shape during cooling. Injection molding is better suited to solid or semi-solid components where the material does not need to stretch into a thin sheet.
Cycle time and throughput
The injection molding process often runs faster for small to medium parts. The material is already packed into the mold, and the cycle is limited by cooling time. For small parts, the cooling time is short, allowing for high throughput.
Blow molding has more steps. The preform must be made, the tube must be heated, the mold must open and close, and the part must be removed. For large parts, the cycle can be longer because the material must stretch further and cool through a thicker section.
Buyers should match cycle time to the part size. A small hollow cup may run faster in a small injection molder because the tooling is compact. A large jug may run faster in a blow molder because the tooling is simple and the part is light. The choice of process depends on the specific dimensions and required production rate.
Tooling cost and changeover
The injection molding process usually requires more expensive tooling. The mold cavity is a finished shape, and it must hold high pressure. Tooling cost is driven by cavity complexity, steel quality, and part precision. Complex features require more machining time and higher-grade steel.
Blow molder tooling is often simpler. The mold is a set of cavities that receive the expanded tube. The tooling cost is lower for basic hollow parts. The mold does not need to withstand the same high pressure as an injection mold, and the geometry is often simpler.
Changeover time matters when running multiple SKUs. A blow molder can change molds quickly if the preform shape is compatible. The blow molding setup can be reduced by using standardized preforms and quick-change mold plates. An injection molder may need more time to change cavities, especially when the part size or material changes. The complexity of the tooling affects the speed of changeover.
Material and quality control
The blow molding process is common for polyethylene, polypropylene, and some copolymers. These materials handle expansion well and produce smooth thin walls. They are chosen for their ability to stretch without tearing.
The injection molding process is wider in material range. It handles engineering plastics, nylon, polycarbonate, acrylic, and many other grades. The material must hold detail and resist deformation during packing. It must also withstand the high pressures involved in filling the cavity.
Quality checks differ. Blow molding parts are checked for wall uniformity, seal integrity, and neck finish. Injection molded parts are checked for dimensional tolerance, surface finish, and feature sharpness. The specific checks depend on the requirements of the part and the application.
A worked example for a buyer
A buyer needs a 2-liter jug for a beverage line. The jug has a thin wall, a wide mouth, and a simple shape. The blow molding process is a natural fit. The preform is small, the mold is a set of cavities, and the part cools quickly because the wall is thin. The thin wall reduces material cost and makes the jug lightweight.
The same buyer also needs a rigid cap. The cap is small, solid, and has a thread. The injection molding process is a better fit. The cap needs tight threads and a smooth surface. A small injection mold can produce the cap at high speed. The injection mold can capture the fine thread detail that would be difficult to achieve with blow molding.
The buyer should not force one process to do everything. The right decision is to match each part to the process that handles its shape best. This approach optimizes cost and quality for each component.
How to choose for your sourcing decision
Use the table below to compare the two processes.
| Factor | Blow Molding | Injection Molding |
|---|---|---|
| Part type | Hollow, thin-wall containers | Solid, thick-wall, detailed parts |
| Wall thickness | Thin, even walls | Variable, often thicker |
| Cycle time | Moderate, varies with part size | Fast for small parts |
| Tooling cost | Lower for basic hollow parts | Higher for complex cavities |
| Material range | PE, PP, some copolymers | Wide range of engineering plastics |
| Changeover | Quick with compatible preforms | Slower with complex molds |
The table is a starting point. The final decision depends on your part list, production volume, and quality requirements. Review each part individually to determine the best fit.
Practical checks before ordering
Before selecting a process, run these checks.
- Send the 3D model to a machine vendor and ask which process fits each part.
- Request samples of both processes if the part is borderline.
- Confirm the material grade and whether it is available in both processes.
- Check the tooling lead time and the expected cycle time.
- Review the sample for surface finish, wall uniformity, and dimensional fit.
The goal is to avoid a mismatch that causes rework or slow production. A clear sample evaluation saves time before tooling is cut.
Common mistakes to avoid
Buyers often choose a process based on cost alone. A low tooling cost for a blow molder does not mean it is the right choice if the part needs fine detail. An injection mold can be expensive, but it may be the only way to meet the design.
Another mistake is ignoring the preform for blow molding. The preform shape affects the part quality. If the preform is wrong, the part may have weak spots or poor neck finish. The preform must be designed to match the final part geometry.
A third mistake is assuming one machine can do everything. A plant may need both a blow molder for jugs and an injection molder for caps. Buying only one type of machine can limit your options. Consider the full range of parts needed for the application.
Final selection
The blow molding process is best for hollow parts with thin walls and simple shapes. The injection molding process is best for solid parts, thick walls, and high-detail features. The right choice is not the cheapest machine. It is the process that matches the part, the material, and the production goal.
Send your part drawings to a vendor. Ask for a process recommendation. Ask for samples. The answer will be clear once the part is in front of you.
Frequently asked questions
Can a blow molder make small solid parts?
No. The blow molding process is designed for hollow parts. Solid parts are better made in an injection molding process.
Which process is cheaper for a thin-walled bottle?
The blow molding process is usually cheaper for thin-walled bottles because the tooling is simpler and the material usage is low.
Can I use the same material in both processes?
Some materials like polyethylene and polypropylene work in both. The injection molding process uses a wider range of engineering plastics.
How do I know which process to choose for a new product?
Send the 3D model to a machine vendor. Ask which process fits the part shape, wall thickness, and production speed.
What is the biggest difference between the two processes?
The blow molding process shapes the part by inflating a tube. The injection molding process packs material into a finished mold cavity.