Blow Molder Buyers Guide: Preform Stretching and Wall Uniformity
To select a reliable blow molding machine, verify how the stretch cycle controls preform stretching and how the system maintains wall thickness uniformity. Focus on mold temperature stability, cylinder pressure control, and post-stretch cooling to ensure consistent container quality.
- Preform stretching determines how material moves before gas inflation, directly affecting final wall distribution.
- Wall thickness uniformity depends on synchronized cooling, cylinder pressure, and mold temperature control.
- Inspect the machine's ability to hold tight tolerances during high-speed production runs.
- Match the blow molder's cylinder and gas control capabilities to your specific resin and container geometry.
Why Wall Thickness Drives Selection
Hollow containers fail when walls are too thick, too thin, or uneven. A buyer evaluating a blow molding machine must look beyond tonnage and speed. The core question is whether the machine can hold the wall thickness uniformity required by the product.
In practice, this means checking the blow molding machine’s ability to manage the preform, stretch it, and inflate it without hot spots or thin zones. A machine that produces beautiful samples but drifts after an hour is not a production asset. You need a system that holds the same wall profile through a full shift.
The two variables that matter most are preform stretching and the final wall thickness uniformity. These are not separate checks. They are linked. If the preform stretches unevenly, the gas inflation will never fix the problem. The final container will carry the defects from the earlier stages.
Consider a standard beverage bottle. If the stretch zone pulls the parison too hard on one side, the material thins there. When the gas inflates the bottle, the thin area stays thin. The gas fills the volume, but it does not redistribute the resin. The result is a bottle that fails pressure tests. The buyer must treat the stretch process as the foundation of quality control. Without it, the inflation step is just a gamble on the final geometry.
How Preform Stretching Works in the Cycle
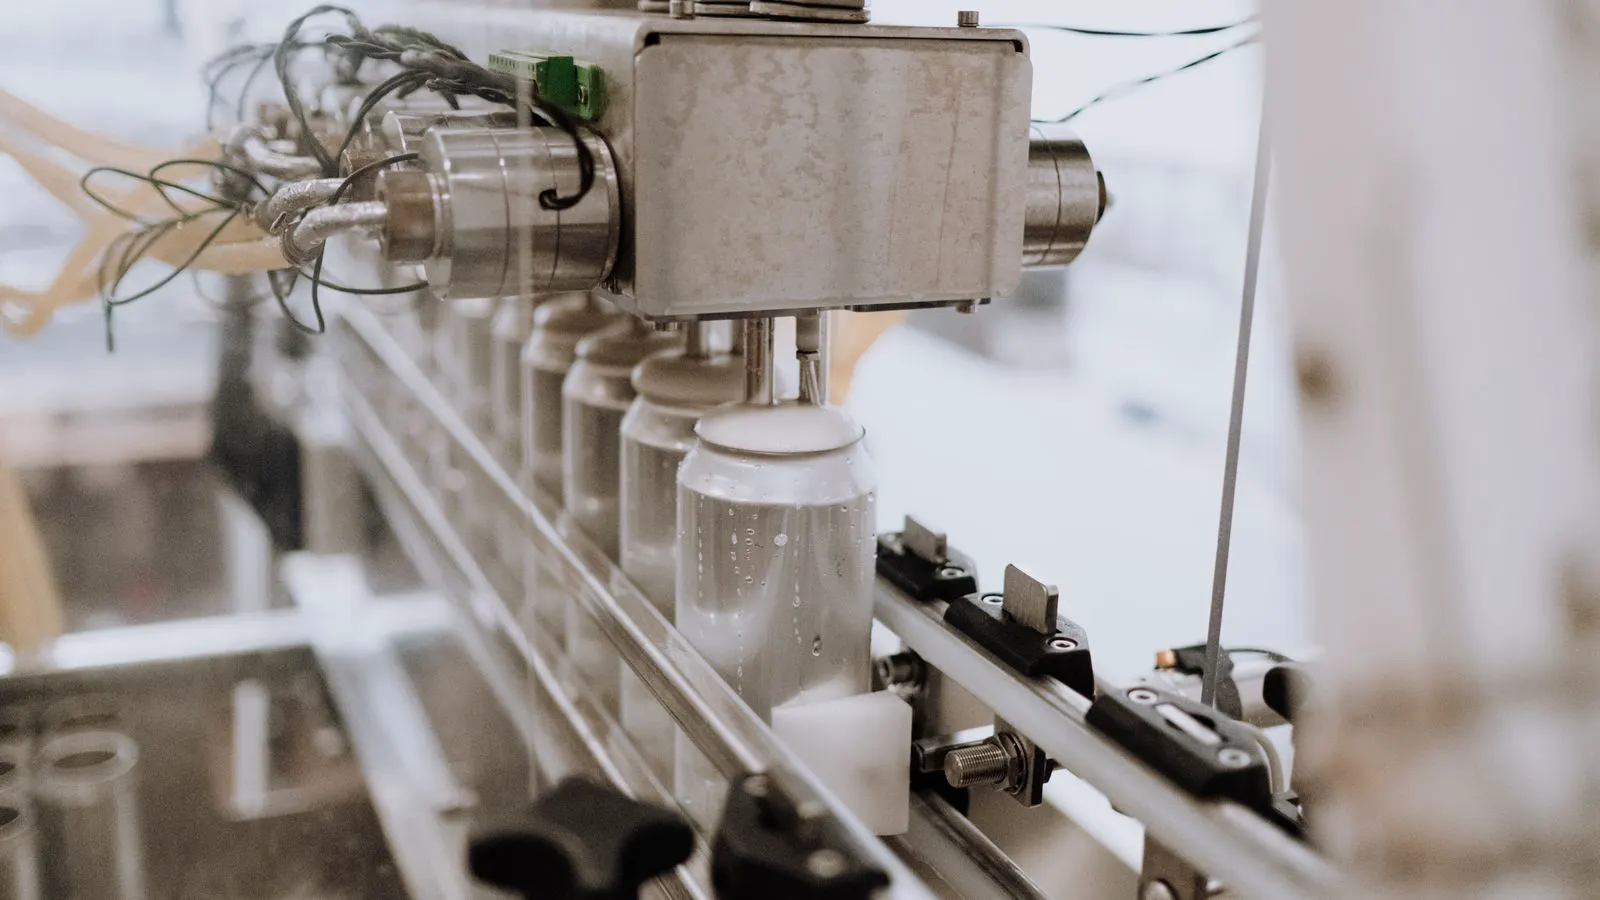
Preform stretching happens between the parison cooling and the mold closure. The preform hangs in a stretch zone. The machine pulls the parison down or applies a pulling force. This moves the material into the mold cavity.
The stretch force determines how the material thins and orients. A strong stretch thins the preform faster. This helps the machine fill deep cavities or complex shapes. But it also increases the risk of thin spots if the force is too high.
When you visit a factory floor, watch the parison exit the stretch zone. The material should move smoothly. If you see the parison wobble, or if the stretch force changes between cycles, the wall thickness uniformity will suffer.
The blow molder must control the stretch time and force independently. A basic machine may use a fixed timer. A better machine uses pressure or position sensors to confirm the parison is at the right location before the mold closes. This consistency is what prevents the thin zones that appear at the bottom of bottles.
Think about the mechanics of the pull. The parison is a tube of semi-liquid resin. As the machine pulls it, the diameter shrinks and the length grows. This action orients the polymer chains along the direction of the stretch. Proper orientation improves the strength of the final wall. If the pull is jerky or uneven, the chains orient randomly in some areas. The wall becomes weak in those spots.
There are different ways to achieve the pull. Some machines use a mechanical grip that moves the parison downward. Others use a suction cup that lifts the parison upward while the mold moves downward. The method changes the load on the resin. A suction lift can create a vacuum effect that pulls the material differently than a mechanical grip.
You must check how the stretch zone is heated. The resin needs to be plastic enough to stretch without breaking. If the stretch zone is too cold, the parison may tear or stretch unevenly. If it is too hot, the parison may slump before the stretch begins. The temperature profile of the stretch zone must match the resin type. This is often overlooked during initial evaluations.
Mold Temperature and Wall Thickness
The mold holds the parison during inflation. The mold temperature controls how fast the resin cools. If the mold is too hot, the resin stays fluid for too long. The gas pressure pushes the material into thin spots. If the mold is too cold, the resin solidifies too fast. The material cannot move to fill the cavity.
A well-designed blow molding machine keeps the mold temperature steady. You should ask about the mold temperature control system. Does it use a single zone? Or does it use multiple zones to handle different parts of the mold?
Complex containers need multiple zones. A bottle with a long neck and a wide body needs different cooling rates. The neck needs to cool faster to prevent flashing. The body needs to cool slower to allow the material to flow.
If the machine cannot adjust these zones, the wall thickness uniformity will be inconsistent. The neck may be thin. The body may be thick. This wastes material and makes the product harder to fill with a consistent volume.
The mold temperature affects the final skin thickness. The outer surface of the bottle touches the mold first. If that surface cools rapidly, it forms a rigid skin. The inner core of the resin remains fluid longer. This creates a gradient in material properties. A thick skin can make the bottle brittle. A thin skin can allow the gas to push too hard, creating thin zones.
Check the heating elements inside the mold. Some molds use bands of heating wire around the neck. Others use blocks that cover the entire body. The distribution of heat matters. A poorly designed mold might have hot spots where the heating elements are too close together. These spots keep the resin fluid longer, leading to thicker walls in those areas.
Also consider the cooling medium. Most machines use water or oil. Water cools faster than oil. If the mold is designed for oil, using water can cool it too quickly. This changes the wall thickness profile. The buyer must ensure the utility system matches the mold design.
The mold temperature also affects the release of the finished container. If the mold is too cold, the container may stick to the mold. Forcing it out can scratch the surface or thin the wall further. A well-controlled mold temperature ensures a clean release.
Cylinder Pressure and Gas Control
The cylinder pressure controls how much the preform moves into the mold. This is different from the gas pressure. The cylinder is the mechanical force. The gas is the inflation force. They must work together.
A high cylinder pressure can force the material into tight corners. But it can also stretch the walls too thin. A low cylinder pressure leaves the material in a relaxed state. The gas then has to do more work.
The blow molding machine must allow fine control of both. You want a machine that can make small adjustments without changing the whole process. If you need to stop the line to change a setting, the machine is not flexible enough.
Check the control system. Does it allow you to set the cylinder pressure in small increments? Can you save different profiles for different products? Can you monitor the pressure in real time? These features make the difference between a machine that works and a machine that requires constant attention.
The interplay between cylinder and gas pressure is delicate. If the cylinder pushes too hard and the gas pressure rises too quickly, the walls can thin rapidly. This is often called over-stretching. The resin reaches its limit and may not recover. The final bottle may have a rough texture or weak points.
Conversely, if the cylinder pressure is too low, the parison may not reach the bottom of the mold cavity. The gas then inflates the upper part of the bottle, leaving the bottom with a thick, unformed wall. This thick bottom uses extra material and may look like a defect to the customer.
The timing of the gas pressure is just as important as the amount. The gas should be introduced after the cylinder has positioned the parison correctly. If the gas starts too early, it pushes the resin before it is in the right place. If it starts too late, the resin may cool too much to flow properly.
Modern control systems can sequence these events precisely. They can hold the cylinder pressure at a set level while the gas pressure ramps up. This allows the resin to flow into the corners before the walls thin out. The buyer should look for machines that offer this kind of sequenced control.
Evaluating the Machine for Your Application
Not every product needs the same level of control. A simple cup may tolerate more variation than a pharmaceutical bottle. But the principles are the same. You need to match the machine to the product.
Start with the product. What is the wall thickness? Where are the thin spots? Where are the thick spots? How much variation is allowed? Write these numbers down. They are your acceptance criteria.
Then look at the machine. Can it achieve those numbers? Can it hold them over time? Can it handle the resin you plan to use? Some resins are sensitive to temperature. Others are forgiving. The machine must match the resin.
A practical test is to ask for a trial run. Bring your preform. Run the product for several hours. Measure the wall thickness at multiple points. Check the variation. If the numbers stay within your range, the machine is a candidate. If they drift, walk away.
The trial run is where the real performance shows. The first few dozen bottles are often adjusted by the operator. The quality of the machine is revealed after the first hour. Does the wall thickness stay consistent? Does the cycle time remain stable? Does the machine handle the resin without forming droplets or voids?
You should also test the machine with the worst-case resin. If you use a blend with recycled content, the machine must handle the higher variability. If you use a high-impact resin, the machine must handle the higher melt flow. The trial run should use the exact material you plan to use in production. Do not substitute a generic resin for the test.
Measure the wall thickness at specific points. The bottom of the bottle, the neck, the shoulder, and the body are critical areas. Use a calibrated micrometer or a laser measurement tool. Record the data. If the variation is outside your tolerance, the machine is not ready.
Also check the cycle time. A machine that runs fast but produces defects is not faster. It is just more expensive. The true cycle time includes the time to adjust settings and clean the molds. A machine with quick changeover features can save time in the long run.
Criteria Table for Evaluation
| Criterion | What to look for | Why it matters |
|---|---|---|
| Stretch Zone Control | Adjustable stretch force and time | Ensures even material movement before inflation |
| Mold Temperature Zones | Multiple independent zones | Allows different cooling rates for complex shapes |
| Cylinder Pressure | Fine adjustment and monitoring | Controls material flow into tight cavities |
| Gas Pressure | Stable and consistent supply | Prevents thin spots from over-inflation |
| Control System | Saveable profiles and real time data | Reduces setup time and maintains quality |
| Resin Compatibility | Ability to handle your specific resin | Prevents processing defects and waste |
Decision Checklist
Before you sign a contract, run this checklist. It is the final step to ensure the blow molding machine will deliver.
- Confirm the machine can produce the exact wall thickness profile of your product.
- Verify the mold temperature control has enough zones for your container shape.
- Check the cylinder pressure control for fine adjustment and stability.
- Run a trial with your resin and preform for at least a full shift.
- Measure wall thickness uniformity at multiple points and compare to your specs.
- Ask the supplier how they support process changes when you switch products.
- Confirm the machine’s utility requirements match your plant.
If the machine passes these checks, it is ready for your production line. If it fails, the defects will show up in your product. You will spend more time fixing the product than making it. Choose the machine that gets the walls right from the start.
Frequently asked questions
How do I know if the preform stretching is causing thin spots?
Thin spots usually appear at the bottom of the container or in areas with high curvature. If the stretch force is too high, the material thins too much before the gas inflates it.
Can I fix wall thickness uniformity with the gas pressure alone?
No. The gas pressure helps inflate the mold, but it cannot fix uneven material distribution. You need to control the preform stretching and mold temperature first.
What is the best way to test a machine before buying?
Run a trial with your specific resin and preform. Measure the wall thickness at multiple points over a full production run. Check if the variation stays within your tolerance.
Do all blow molding machines have the same level of control?
No. Basic machines have fixed settings and limited mold zones. Advanced machines have multiple temperature zones, fine pressure control, and data logging. Choose based on your product complexity.
How often should I check the wall thickness?
Check it at the start of every shift and periodically during production. Use a gauge or an inline sensor. If the numbers drift, stop and investigate the cause.