Buyers Guide: Sizing Heat Exchangers for Extrusion
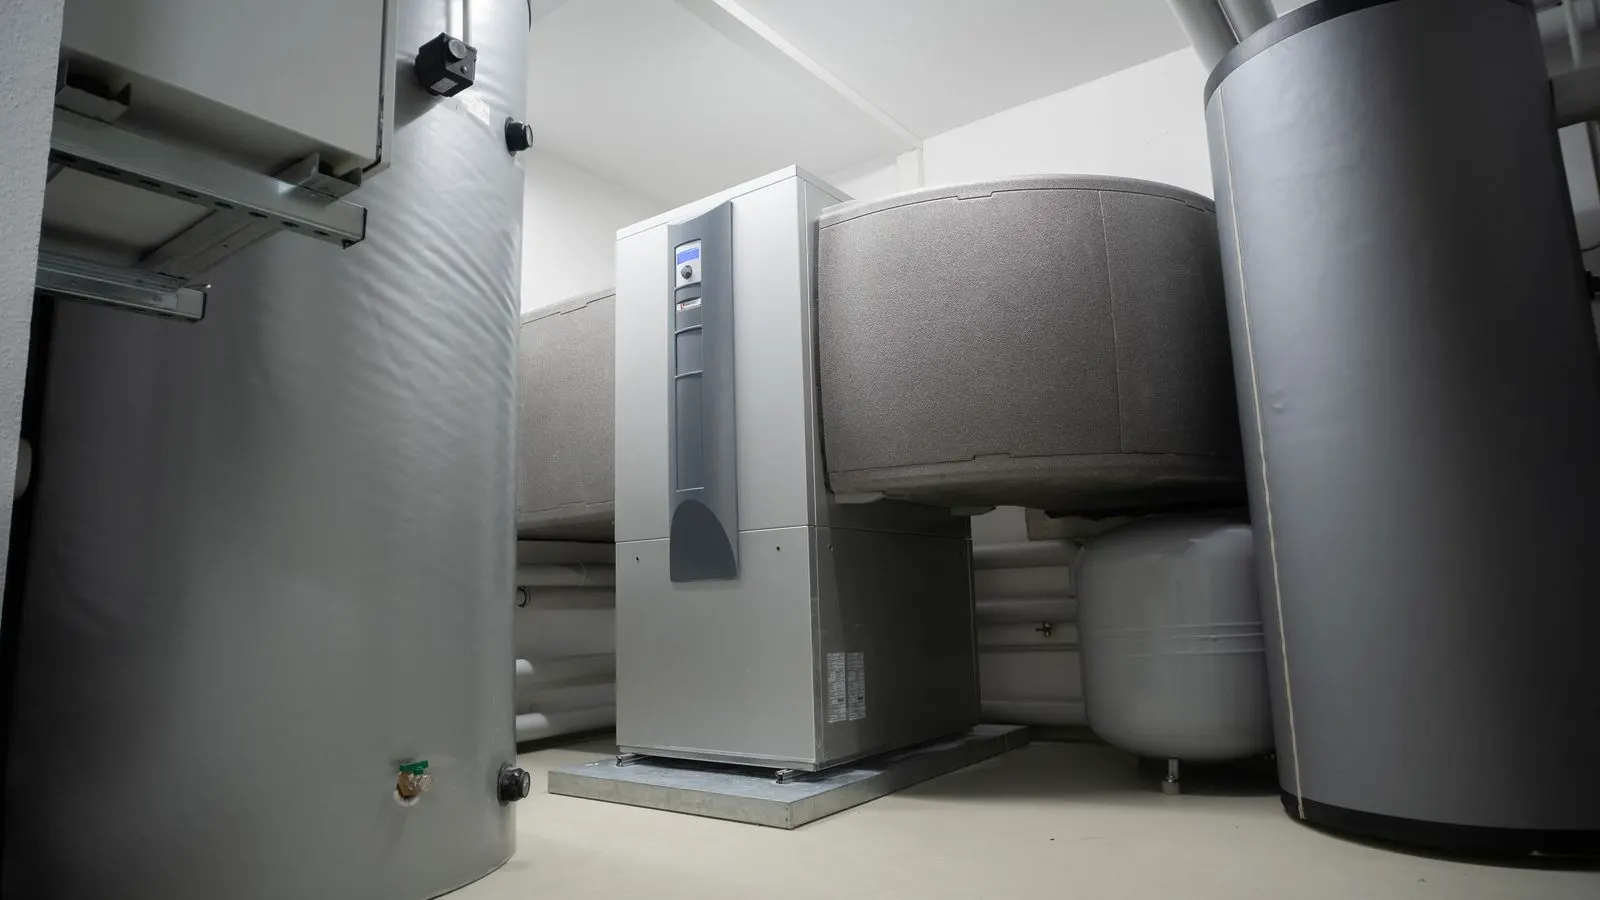
Match heat exchanger capacity to extruder throughput and melt temperature to prevent thermal degradation and reduce energy consumption. Proper sizing improves product consistency and extends equipment life. Evaluate flow rate, temperature differential, and material compatibility before selection.
- Match heat exchanger flow capacity to extruder output to maintain stable melt temperature.
- Insulate heat exchangers to reduce heat loss and lower energy consumption.
- Select materials compatible with the specific plastic being processed.
- Monitor pressure drop to ensure the system does not restrict extruder flow.
- Regular maintenance prevents fouling and maintains thermal efficiency.
Understanding the Role of Heat Exchangers in Extrusion
Heat exchangers manage melt temperature and cooling rates in extrusion lines. They remove excess heat from the polymer after it passes through the barrel and die. Proper sizing ensures the melt reaches the target temperature for downstream processes like cooling, cutting, or forming.
Poorly sized units cause problems. If the exchanger is too small, the melt remains too hot. This leads to degradation, discoloration, or inconsistent product dimensions. If it is too large, the melt cools too quickly. This can cause cold shots, poor layer bonding, or increased shear in the extruder.
The goal is balance. You need a unit that removes the right amount of heat at the right speed. This directly impacts energy efficiency and product quality. Consider a PVC pipe line where the melt exits the die at 200 degrees Celsius. The target temperature at the cooler inlet might be 160 degrees Celsius. The exchanger must remove enough heat to hit that target without chilling the polymer skin before the core cools uniformly. If the unit removes heat too aggressively, the outer layer sets while the inner core remains soft. This mismatch causes warping or poor dimensional stability in the final pipe. Conversely, if the unit is undersized, the melt enters the cooling bath too hot. The polymer may stick to the cooling water pipes or the die itself, creating scrap or inconsistent wall thickness.
Calculating Required Heat Removal Capacity
Start with the mass flow rate of the plastic. Measure the extruder output in kilograms per hour. Multiply this by the specific heat capacity of the plastic. Then multiply by the temperature difference between the melt entering the exchanger and the desired exit temperature.
This calculation gives you the required heat removal rate in kilowatts. A common mistake is using the feed temperature instead of the actual melt temperature. Always measure the temperature at the exit of the barrel or the inlet of the exchanger. For example, if you are processing polypropylene, the specific heat capacity is typically around 1.9 kilojoules per kilogram per degree Celsius. If your line runs at 1,000 kilograms per hour and you need to drop the temperature from 220 degrees Celsius to 180 degrees Celsius, the calculation looks like this: 1,000 kg/h multiplied by 1.9 kJ/kg.K multiplied by 40 K. Convert the flow rate to kilograms per second (approximately 0.278 kg/s) and the result is roughly 21 kilowatts of heat to be removed.
Consider the cooling medium. Water, oil, or air all have different heat transfer coefficients. Water generally provides higher efficiency than air for the same volume. If you use water, account for the flow rate and temperature rise of the cooling water. A water loop with a 5 degree Celsius rise is a standard design parameter. If the flow rate is too low, the water temperature will climb, reducing the temperature difference between the melt and the cooling water. This lowers the heat transfer rate and may prevent the melt from reaching the target exit temperature. Always verify the cooling water flow rate during commissioning.
Matching Flow Rates and Pressure Drop
The heat exchanger must handle the volumetric flow rate of the melt without causing excessive pressure drop. High pressure drop increases the load on the extruder motors. It also reduces the actual throughput of the line.
Check the manufacturer’s pressure drop curves. Compare them against your extruder’s operating pressure. You want a pressure drop that is a small fraction of the total system pressure. A typical target is less than ten percent of the barrel pressure. For a standard single-screw extruder operating at 50 bar of back pressure, the heat exchanger should not add more than 5 bar of resistance. If it does, the extruder has to work harder to push the same volume of melt through the die.
If the pressure drop is too high, you may need a larger diameter tube or a shorter exchanger. This increases the footprint but reduces flow resistance. Balance the space constraints of your plant with the hydraulic requirements of the extruder. In compact plants, space is often the limiting factor. You might be forced to use a longer, narrower tube bundle. This increases surface area for heat transfer but also increases friction. Look for designs with smooth internal surfaces and minimal bends. Each bend adds turbulence and pressure loss. Straight flow paths are preferable where space allows. If space is tight, consider a multi-pass design that keeps the total tube length manageable while maintaining adequate heat transfer area.
Material Compatibility and Fouling Prevention
Select materials that resist corrosion and fouling. Stainless steel is a common choice for general plastics processing. However, some plastics contain additives that may react with certain metals. Always check the material compatibility charts provided by the exchanger manufacturer. For instance, certain chlorine-based PVC formulations can be aggressive towards standard stainless steel if the melt temperature is too high or if the residence time is too long. In such cases, higher alloy steels or specialized coatings might be required.
Fouling is a major issue. Residual plastic can build up on the inner walls of the tubes. This reduces the heat transfer surface area and increases pressure drop. Choose a design that allows for easy disassembly and cleaning. A heat exchanger that requires taking the entire unit out of the line for cleaning creates downtime. A design where the tube bundle can be pulled out or the tubes can be accessed without disassembling the whole unit is far more practical. Consider the viscosity of the melt. High viscosity plastics tend to stick to surfaces. They may require higher temperature gradients or specific surface finishes to prevent adhesion. Test the exchanger with the actual material before full production. Run a short trial batch and inspect the tubes afterward. If you see buildup, adjust the surface temperature or consider a different surface treatment.
Evaluating Energy Efficiency and Waste Reduction
Energy savings come from reducing heat loss and optimizing the cooling process. Insulate the heat exchanger and the piping. Use low-temperature insulation to keep the outer surface below a safe touch temperature while minimizing radiative heat loss. A well-insulated exchanger loses less heat to the ambient air. This means the cooling medium does not have to work as hard to remove the same amount of heat from the melt.
Recover the heat from the cooling water. The water leaving the exchanger still contains significant thermal energy. You can use this heat to warm up the incoming plastic pellets or preheat the factory space. This closed-loop system reduces the load on your boiler or electric heaters. For example, if the cooling water exits at 45 degrees Celsius, it has enough heat to warm the plastic pellets from 20 degrees Celsius to 35 degrees Celsius before they enter the extruder. This reduces the energy needed to heat the pellets and lowers the overall energy consumption of the line.
Monitor the energy consumption of the cooling system. The pumps that circulate the cooling medium consume electricity. Use variable speed drives to match the pump speed to the actual flow rate. This reduces energy use during low production periods. If the line runs at half speed, the cooling demand is also lower. A fixed-speed pump will waste energy by pushing more water than necessary. Variable speed drives allow the pump to adjust in real time based on the actual heat load.
Criteria Table for Selecting a Heat Exchanger
| Criterion | What to look for | Why it matters |
|---|---|---|
| Heat Transfer Capacity | Rated in kW, matching your calculated requirement | Ensures the melt cools to the target temperature |
| Pressure Drop | Low at your operating flow rate | Prevents excessive load on the extruder motors |
| Material Compatibility | Stainless steel or other compatible alloys | Prevents corrosion and contamination of the plastic |
| Fouling Resistance | Easy-to-clean design, smooth surfaces | Maintains efficiency over time and reduces downtime |
| Footprint | Fits within your plant space constraints | Allows for proper installation and maintenance access |
| Cooling Medium | Water, oil, or air, with adequate flow capacity | Determines the overall thermal management strategy |
| Control Integration | Supports temperature sensors and control loops | Enables precise temperature control and automation |
Decision Checklist
- Measure the actual melt temperature and flow rate at the extruder exit.
- Calculate the required heat removal in kilowatts using specific heat values.
- Check the pressure drop of the candidate exchangers at your flow rate.
- Verify material compatibility with your specific plastic and additives.
- Evaluate the ease of cleaning and maintenance for the chosen design.
- Inspect the insulation and check for potential heat loss points.
- Plan for heat recovery from the cooling medium.
- Integrate temperature sensors into the control system.
- Test the exchanger with the actual material at full speed.
- Monitor energy consumption and adjust flow rates as needed.
Common Mistakes to Avoid
Sizing the exchanger based on the maximum extruder speed rather than the average production speed. This leads to over-investment in capacity. You may end up with a unit that is too large for most of the time. Consider a line that runs at 80 percent of its maximum capacity for most of the shift. If you size the exchanger for 100 percent capacity, you are paying for extra heat transfer area that will sit idle for a significant portion of the operating time.
Ignoring the thermal mass of the plastic. The plastic itself acts as a thermal buffer. If the exchanger is too small, the melt may remain too hot for a longer period, causing degradation even if the exit temperature is within range. The temperature drop across the exchanger is not linear. The melt cools faster at the beginning and slower near the exit. If the exit temperature is correct but the melt was too hot for the first half of the exchanger, degradation can still occur. This is especially true for heat-sensitive materials like some engineering thermoplastics.
Failing to account for seasonal variations. In summer, the ambient temperature is higher. The cooling water may enter the exchanger at a higher temperature. This reduces the temperature differential and the cooling capacity. You may need a larger exchanger or a chilled water system in hot climates. Design the system for the worst-case summer conditions, not the average annual conditions. If the plant is in a tropical region, the ambient water temperature might be 30 degrees Celsius instead of 15 degrees Celsius. This doubles the required heat transfer area to achieve the same cooling effect.
Neglecting the cooling medium circulation. If the cooling water flow is too low, the temperature of the water increases as it passes through the exchanger. This reduces the effective cooling capacity. Ensure the circulation pump is sized correctly. A common error is sizing the pump for the maximum flow rate but not verifying that the piping and valves allow that flow without excessive pressure loss. If the pump cannot deliver the required flow, the water temperature rise will be higher, and the cooling performance will degrade.
Final Thoughts
Sizing heat exchangers for extrusion is a technical task. It requires accurate measurements and a clear understanding of the thermal dynamics. Get the sizing right, and you will improve product quality, reduce waste, and lower energy costs. Take the time to verify each step of the calculation. A well-sized heat exchanger is a reliable asset that pays for itself in efficiency gains. Do not rely on generic rules of thumb. Each material, each extruder, and each process has its own thermal profile. Measure, calculate, and test. The data will tell you what the system actually needs.
Frequently asked questions
How do I know if my heat exchanger is too small?
If the melt exit temperature is higher than the target, or if the exchanger causes discoloration or degradation, it is likely too small. Check the temperature at the exit of the exchanger.
What is the typical pressure drop for a heat exchanger in an extrusion line?
It varies, but a good target is less than ten percent of the barrel pressure. Check the manufacturer's curves for the specific flow rate and temperature.
Can I reuse the cooling water from the heat exchanger?
Yes, you can recover the heat from the cooling water. Use a secondary heat exchanger to transfer the heat to the incoming pellets or preheat the factory space. This improves overall energy efficiency.
What materials are best for heat exchangers in plastic processing?
Stainless steel is the most common choice. It resists corrosion and fouling. However, some plastics with specific additives may require other materials. Check compatibility charts.
How often should I clean the heat exchanger?
It depends on the plastic and the production schedule. High viscosity plastics may require more frequent cleaning. Monitor the pressure drop. If it increases, clean the unit.